Production Planning Constraints: How to Build Schedules That Match Factory Reality
Build more realistic manufacturing schedules around finite capacity, bottlenecks, material readiness, staffing skills and connected production execution.
Capar Labs21 min readProduction PlanningSchedulingManufacturing
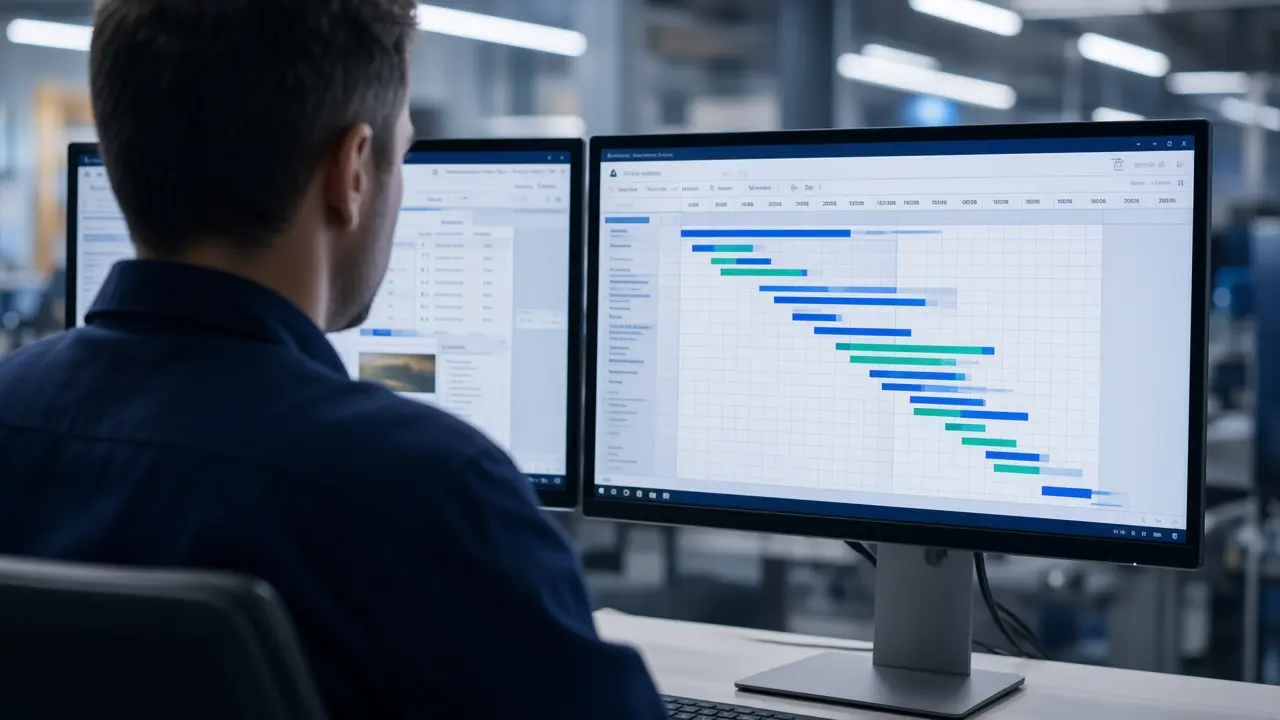
A production planning board can look convincing on Monday morning. Every order has a start and finish date, the machines appear occupied at sensible intervals, and the customer delivery dates are still green.
By Wednesday, the situation is different. A setup takes longer than the engineering estimate. A critical material arrives but has not been released by Quality. A qualified setup technician is absent. Machining finishes late, pushing work toward an assembly department that is already close to full capacity.
The schedule was not necessarily created carelessly. It may have been calculated from data that was technically available but operationally incomplete.
Realistic production planning is the discipline of matching customer demand with the factory's actual resources, readiness conditions, process dependencies and normal variation. It is not simply the act of placing orders into free spaces on a calendar.
The most useful production schedule is one employees can execute, understand and adjust deliberately when circumstances change.
1Why a complete-looking production schedule can still be impossible
Manufacturers frequently start planning with demand, a routing, expected processing times and a calendar. Those are necessary inputs, but they do not fully describe manufacturing readiness.
A machine may be free on paper but unavailable because of planned maintenance. Materials may be recorded in inventory but held for inspection. An employee may be present but not qualified to perform a specific operation. A drawing or manufacturing instruction may still require engineering approval.
A common planning mistake is to treat scheduled, available and ready to execute as equivalent states. They are not.
Consider three questions that should be answered before a job is committed:
Can it be done? Do the required equipment, tooling, people, materials and authorized instructions exist and meet the process requirements?
When can it be done? Is enough genuinely available capacity left after other commitments, setups, planned stops and dependencies?
What will it affect? If we schedule this order here, which other orders, downstream operations and delivery commitments change?
Production scheduling therefore involves more than machine loading. It is a coordination problem across production, engineering, inventory, quality, maintenance and customer demand.
The Association for Supply Chain Management (ASCM) describes capacity management as the process of establishing, measuring, monitoring and adjusting capacity across multiple planning levels, from higher-level requirements to input/output control. That is a useful reminder: a monthly production target and a workable machine-level sequence answer different questions.
Materials
May be in inventory but still awaiting release.
Engineering
A drawing or instruction may still need approval.
Equipment
A machine can appear free yet still be unavailable.
People
An employee may be present but not qualified to run the job.
2Understand the difference between infinite and finite capacity
Infinite vs. finite capacity planning
Infinite capacity (theoretical)
Overload
Order AOrder BOrder C
Illustrative overload — 108% of a period
Finite capacity (realistic)
Feasible
Order AOrder BOrder C
Any unscheduled work remains visible
An infinite-capacity planning calculation can place work into a period even when the combined workload exceeds the capacity actually available. This can be useful for identifying demand pressure or evaluating what additional capacity would be required, but it should not be mistaken for an executable schedule.
Finite-capacity scheduling considers capacity already reserved for other work and looks for an available place for an operation. It can show when the requested completion date is infeasible with current resource assumptions.
Microsoft's documentation of finite-capacity scheduling illustrates this distinction: the available capacity of a resource, existing reservations and the defined operation sequence influence when work can be scheduled.
However, even a finite-capacity schedule can be wrong if the underlying assumptions are wrong. An incorrect cycle time, missing setup, unrealistic staffing assumption or unavailable material can make a mathematically consistent plan impossible to execute.
Finite capacity is not the same as verified feasibility. The model still needs to reflect the factory.
This is why experienced planners distinguish between what a scheduling tool calculates and what the operations team has actually confirmed.
3Start with the constraint that governs the flow
Capacity by operation · illustrative
A
69%
B
115%
C
69%
Operation B needs 46 hours but has 40 hours available.
When a factory has several machines and departments, adding up all available machine hours tells only part of the story.
Suppose an illustrative production route uses three operations:
Operation
Available weekly hours
Required workload
Capacity load
A
80
55
69%
B
40
46
115%
C
70
48
69%
Fictional figures for illustration; percentages are rounded.
Operation B is overloaded by six hours. It is the immediate capacity constraint for this workload. Adding hours to Operation A will not solve that particular shortage if work still has to pass through B.
The planner may need to review the order mix, the real processing time at B, setup opportunities, alternative approved resources or the possibility of adding capacity lawfully and safely.
A constraint is not necessarily a machine. It can be a specialist technician, a tool shared across several machines, a heat-treatment operation, inspection capacity or a required material that arrives too late.
Constraints can also shift. Improving one overloaded operation may reveal another resource as the next limiting factor.
The practical lesson is to manage the production flow through the limiting resource, not just maximize the individual utilization of every machine. Keeping every non-bottleneck machine busy can create excess work-in-progress without increasing completed output.
Lean production guidance makes a related point: production control should consider the pace of the overall value stream, not only the efficiency of separate operations.
4Validate planning times with engineering and shop-floor evidence
A production planning system is only as credible as the times and conditions it uses.
Suppose an engineering routing estimates a cycle time of 30 seconds per component. If the machine and process achieve 38 seconds under normal, approved conditions, a large order may consume substantially more time than the planning board expects.
Before changing the standard, investigate the cause. A longer historical runtime might reflect an incorrect estimate, but it could also include unusual breakdowns, waiting, scrap, additional inspection or a different product variant.
A useful validation method combines three sources:
Engineering definition. Check the approved routing, expected cycle time, batch size, setup method and production conditions.
Historical execution. Compare previous orders for the same or a comparable article. Separate active production time from setups, planned stops, interruptions and reporting inaccuracies where possible.
Physical observation. Speak with operators and technicians, observe actual setups and cycles, and investigate differences between the recorded data and the work being performed.
This is not a contest between engineers and operators. Both perspectives are necessary. Engineering supplies a controlled process definition; production experience tests whether the planning assumptions describe that process accurately.
Where a process changes, the relevant planning master data should be reviewed and updated through the company's defined responsibilities.
5Count the entire operation—not just the time a machine produces parts
Example: an eight-hour production window
Setup and preparation 60 minProduction running 360 minCleaning and changeover 30 minPlanned stops or other allowance 30 min
Illustrative allocation. Actual shift availability depends on the process and working arrangements.
A frequent source of planning error is treating the whole shift as available production time.
Manufacturing orders can require preparation, material staging, tooling setup, first-piece approval, running time, sampling, cleaning and changeover. They may also share resources with other work.
Consider an illustrative eight-hour scheduled production window:
Activity
Duration
Setup and preparation
60 minutes
Productive running
360 minutes
Cleaning and changeover
30 minutes
Planned stops or other allowance
30 minutes
Total window
480 minutes
Illustrative allocation, not a universal shift standard. Breaks, paid time and available production hours depend on the applicable arrangements and the actual process.
If a planner models eight hours of pure running time, the expected output may be overstated.
The opposite error is also possible: a planning model may assume every setup activity must stop the machine when some preparation can happen beforehand.
The Lean Enterprise Institute's explanation of SMED (Single-Minute Exchange of Die) highlights the distinction between internal setup activities, which require equipment to be stopped, and external setup activities that can be completed while equipment is running.
For example, preparing the next tool and staging material may be possible before the current order ends, subject to the factory's procedures. Reducing avoidable setup time can improve available capacity without pretending that the machine has more hours in the day.
Cleaning deserves particular care. It may be a time requirement within or between manufacturing operations rather than an independent operation in the product routing. How it is represented should match the actual process and approved documentation.
Accurate scheduling depends on the total time and resource requirements of each operation—not just nominal machine cycle time.
6Plan with the actual skills available, not a headcount
A factory may have six available machines and six employees, yet lack the capability to run six operations at the same time.
An operation may require a qualified setup technician, a certified inspection activity, specialist tooling knowledge or a trained person who can supervise a particular process.
Staffing capacity therefore has several dimensions: available hours, required qualifications, skill distribution, supervision requirements and the extent to which people can safely cover multiple activities.
A practical example is a technically qualified employee performing setups across several machines while other authorized employees run established production. Another possibility is supervising two compatible long-cycle operations when the process permits it and safety and quality controls are maintained.
Neither arrangement should be assumed universally safe or appropriate.
The planning process needs to distinguish available staffing capacity from assigning a specific named person to a machine or task. Qualification information can help determine whether a schedule is realistic, while day-to-day responsibility for individual assignments may belong to supervisors or another approved staffing process.
Overtime also needs caution. More working hours are not automatically more safe or productive capacity. Research and guidance from the US Occupational Safety and Health Administration (OSHA) identify fatigue-related risks associated with long and irregular work schedules.
The correct question is not merely “Can someone stay longer?” It is “Can the required work be performed competently, safely and within the applicable working-time rules?”
7Separate physical material availability from production readiness
A delivery date on a purchase order is not the same as a confirmed material-ready date.
Consider a component expected to arrive on Wednesday morning. The item may still need to be received, identified, inspected, released or transported to the relevant workstation.
For realistic scheduling, it helps to distinguish:
Material state
Planning meaning
Expected from supplier
An estimate or commitment, not physically available
Received in warehouse
On site, but possibly awaiting processing or inspection
On quality or other hold
Not available for affected use until appropriately released
Released and unallocated
Potentially available, subject to location and quantity
Reserved or staged for an order
More specific readiness evidence for the planned work
Engineering readiness creates a similar challenge. A drawing or manufacturing instruction may be undergoing revision. A manufacturing order might have sufficient material and machine capacity but still lack the approved documentation needed to proceed.
The planner should see relevant holds and readiness information in a form they can interpret, without treating a forecast release date as proof of authorization.
In regulated and tightly controlled manufacturing, approved operating conditions, personnel competence and product conformity may impose further restrictions on equipment or process substitutions. Applicable obligations depend on the industry and the manufacturer's quality system.
An order is ready only when the conditions required for its execution are satisfied—not merely when its materials appear somewhere in inventory.
8Plan the whole routing and its downstream consequences
01Cutting
02Machining
03Assembly
04Quality Control
A manufacturing schedule is more than a collection of independent machine calendars.
Imagine the following route:
Cutting → Machining → Assembly → Quality Control
If machining finishes late, assembly may start late. If quality control follows assembly, product release and final delivery may be affected in turn.
But that outcome is not inevitable. Assembly may have unallocated time, another order may finish early, or the delayed operation may have sufficient scheduling flexibility to absorb a modest variation.
This is why the severity of a production delay cannot be judged by minutes late alone. It depends on the downstream sequence, resource loading, shared tooling, required inspections, customer commitments and the amount of usable time remaining.
A useful distinction is between operation delay and delivery risk. One operation can be late while the final shipment remains achievable. Another operation can be only slightly late but immediately block a heavily loaded downstream bottleneck.
NIST research on simulation-integrated production planning explains that static planning assumptions can become infeasible as shop-floor events change and that evaluating realistic shop-floor resource conditions can improve planning decisions.
The management lesson does not require sophisticated simulation software. Even a simple visual route and dependency review can help planners recognize whether a local delay has become a system-wide problem.
9Make room for variability without filling every minute
A schedule calculated to use every minute of every critical resource has almost no room to absorb normal variation.
Actual setups may take longer than expected. Equipment may stop briefly. Inspection may require an additional check. A supplier may deliver late. A previous operation may complete early.
The planner needs to decide where limited flexibility is most valuable.
Depending on the process, that might involve a manageable time allowance, carefully chosen work-in-progress buffers, alternative approved capacity or a sequence that avoids unnecessary changeovers.
Buffers should be deliberate. Excessive work-in-progress can hide problems, consume floor space and extend lead times. Likewise, indiscriminately inserting time into every operation can make the schedule unnecessarily slow.
Lean's heijunka concept addresses the value of leveling production mix and volume in suitable environments, reducing the disruptive effect of large swings in what a production process is asked to do.
There is no single scheduling rule that fits a high-mix machine shop, a repetitive assembly line, a batch-process facility and a regulated cleanroom. The appropriate amount and location of flexibility depend on demand patterns, changeover economics, process stability and customer requirements.
The objective is not a schedule with zero idle time. It is a stable production flow that can meet its commitments.
Good reasons to include flexibility
Setup may take longer than the standard
Equipment may stop unexpectedly
Inspection can require extra checks
Supplier delivery estimates can change
Avoid excessive buffers
Unnecessary work-in-progress
Additional inventory and floor space
Longer manufacturing lead times
Problems hidden rather than resolved
Examples illustrate scheduling trade-offs, not universal operating targets.
10Keep planning connected to actual shop-floor execution
When a factory operates 20 or 30 machines, a planner cannot continuously verify each operation by physically visiting the entire floor.
A visual planning board can provide a useful overview of planned orders, operation sequences, actual progress and relevant constraints. But its value depends on current, credible information.
For example, operators may have finished a job without reporting completion. A machine may have stopped without a timely record. A shift may have handed over unfinished work but not updated the order status.
A visually impressive plan can therefore become unreliable within hours.
The international ISA-95 / IEC 62264 standards family provides a useful framework for distinguishing business planning from manufacturing operations management and for describing the information exchanged between those functions. It does not require all planning and execution functions to reside in one application.
A connected workflow should enable planners to compare scheduled, in progress, completed and restricted activities using consistent definitions. The system should also preserve enough history to understand why the plan and the execution diverged.
The operational goal is not to collect the most data. It is to provide the information needed for the next sound decision.
11Not every delay deserves a new schedule
Respond to impact, not delay alone
Monitor
20 minutes late; the next operation still has usable time.
Evaluate
Two hours late; downstream assembly is already heavily loaded.
Illustrative scenarios, not universal thresholds.
Production planning often suffers from two opposite behaviors: ignoring real problems too long, or reacting to every small deviation by rearranging the whole plan.
A more useful trigger for intervention is the likely consequence of a deviation.
Situation
Potential consequence
Sensible initial response
Operation A is 20 minutes late, and the next operation has available time
Little immediate downstream effect
Monitor the existing plan
Operation B is two hours late and blocks an overloaded assembly resource
Multiple orders could be affected
Investigate alternatives promptly
Operation C is four hours late, but the final commitment has sufficient verified flexibility
No current delivery risk
Monitor while validating the remaining assumptions
Illustrative situations. Time alone does not define an intervention threshold.
Changing the sequence of orders can cause additional setups, material movements and confusion for supervisors. If adjustments occur constantly, employees may no longer know which version of the schedule to follow.
A practical operating rhythm can distinguish a relatively stable near-term execution schedule from a longer-term plan that remains easier to adjust. Exceptions still need a defined way to be reviewed and approved.
A stable schedule is valuable, but stability is not the same as refusing to respond to real operational risk.
12Evaluate recovery options in the context of the entire factory
When a delay cannot be absorbed, a planner may have several choices. Each has benefits and consequences.
Extend available working time
An extra shift, overtime or weekend work may recover capacity with fewer equipment changes. But it can increase cost, fatigue exposure and support-function requirements. Extra production hours are useful only if the needed operators, maintenance, materials and inspection resources are also available.
Use an alternative qualified resource
Another machine may have capacity, but moving work can require tooling changes, setups, process verification, revised documentation or customer/quality approval where applicable. An available machine is not automatically a suitable machine.
Change the order sequence
Sequencing compatible jobs together may reduce setup time. However, prioritizing setup efficiency at the expense of an urgent customer delivery may be a poor trade-off. The planner must compare the wider impact.
Adjust the delivery commitment
If a realistic recovery is not feasible, Planning should communicate the risk to the appropriate commercial function early enough to manage customer expectations. A single delayed component may prevent an entire multi-item customer order from shipping.
A disciplined decision compares which alternatives are technically possible, lawful, safe and commercially sensible—then records the selected schedule change and communicates it to the people who must execute it.
Replanning is a management decision, not a software side effect.
13What manufacturing standards and European working-time rules mean for planning
Good planning must be consistent with the controls under which the factory operates.
Quality-management and production controls
ISO 9001:2026, published on September 16, 2026, is the current edition of the widely used quality-management standard. It preserves the focus on process control, risk-based thinking and continual improvement while emphasizing leadership and quality culture.
For production planning, the practical implication is that schedule pressure should not override approved production conditions, necessary competence, quality checks or appropriate authorization. ISO 9001 is a management-system standard rather than a universal manufacturing scheduling law. Certification and transition arrangements depend on the organization and its certification body.
Additional sector-specific requirements may apply in medical devices, pharmaceuticals, aerospace or other regulated manufacturing. Manufacturers should evaluate those rules before substituting equipment, shortening required process steps or changing approved methods.
Working time and overtime in the EU
The EU Working Time Directive (2003/88/EC) provides common minimum protections, including an average maximum working week of 48 hours including overtime, at least 11 consecutive hours of daily rest in each 24-hour period, and rules on weekly rest and breaks.
These are minimum EU-level requirements with implementation details, reference periods and possible derogations or opt-outs depending on the circumstances and national law. Collective agreements and national rules may provide additional protections.
A planning manager evaluating overtime must therefore check the applicable national legislation, collective arrangements and individual working-time circumstances—not assume that any employee can simply add another shift.
Safety and fatigue remain considerations even where an overtime arrangement is legally permitted. OSHA's guidance identifies reduced alertness and increased safety risk as concerns with long or irregular work schedules.
Production deadlines do not remove legal, safety or quality obligations.
14Measure planning effectiveness—not only machine utilization
A schedule should be evaluated by whether it helps the factory deliver reliable outcomes, not just by whether the planning board appears full.
A small, carefully defined set of measures can help:
Measure
What it helps reveal
Schedule adherence
Whether operations begin and finish in line with agreed plans
Load versus available capacity
Where over-commitment or unbalanced resources persist
Planned versus actual processing and setup time
Which time standards need verification
Bottleneck throughput
Whether the limiting resource supports required output
Work-in-progress and waiting time
Where work accumulates between operations
Order completion and on-time delivery
Whether the schedule supports customer commitments
Rescheduling frequency and reasons
Whether data, instability or decisions are creating unnecessary change
Measures need clear definitions. For example, “completed” might mean the operation was physically finished, or it might mean the product passed required quality checks. Those are different events and should not be mixed.
ISO 22400 provides a framework for defining manufacturing operations KPIs. Its published Part 2 describes indicator formulas and characteristics, while a revised edition is under development as of October 2026.
The aim is to learn from deviations, not punish employees for reporting the truth. If the planning data is consistently inaccurate, improving the data may deliver more value than adjusting the planning algorithm.
92%Schedule adherence
38 minSetup time variance
94%On-time delivery
78%Machine utilization
Illustrative indicators. Definitions must match the factory's actual events, not mixed statuses.
15A practical way to improve production scheduling
Manufacturers do not need to begin with an expensive, factory-wide technology replacement.
A focused improvement can start with one product family, one overloaded resource or one recurring planning failure.
First, observe the actual workflow. Review production orders, interview operators and planners, and identify the gap between the schedule and real execution. Look particularly at the bottleneck and its supporting resources.
Second, correct the planning assumptions. Check routings, real cycle times, setup and cleaning allowances, working calendars, skills requirements, material statuses and approved process restrictions.
Third, build an executable sequence. Load the important resources according to genuinely available capacity and connect the order's dependent operations. Make the assumptions and unresolved risks visible.
Fourth, agree on execution and exception handling. Ensure employees understand the schedule, know how to record progress and know who is authorized to change priorities when disruptions occur.
Finally, verify with real orders. Compare planned and actual results over representative periods, learn from deviations and improve the model before expanding to other areas.
This approach respects a principle found throughout operations improvement: technology is most useful when it reinforces a sound process rather than attempting to compensate for an undefined one.
16Where connected manufacturing technology fits
Manufacturing planning becomes more dependable when relevant information is connected across planning, shop-floor execution, inventory, quality, maintenance and workforce processes.
A planning system can help present machine loads, relevant constraints, operation dependencies and execution updates. Depending on the software and its verified capabilities, it may also help a planner evaluate alternatives or review proposals.
But the presence of a visual planning board does not prove that its input data is accurate. Nor should the application silently change priorities or override approved production restrictions.
At Capar Labs, we support manufacturers with production planning and operations consulting, manufacturing process improvement, industrial data and systems integration. That work can involve improving existing tools, not only introducing new software.
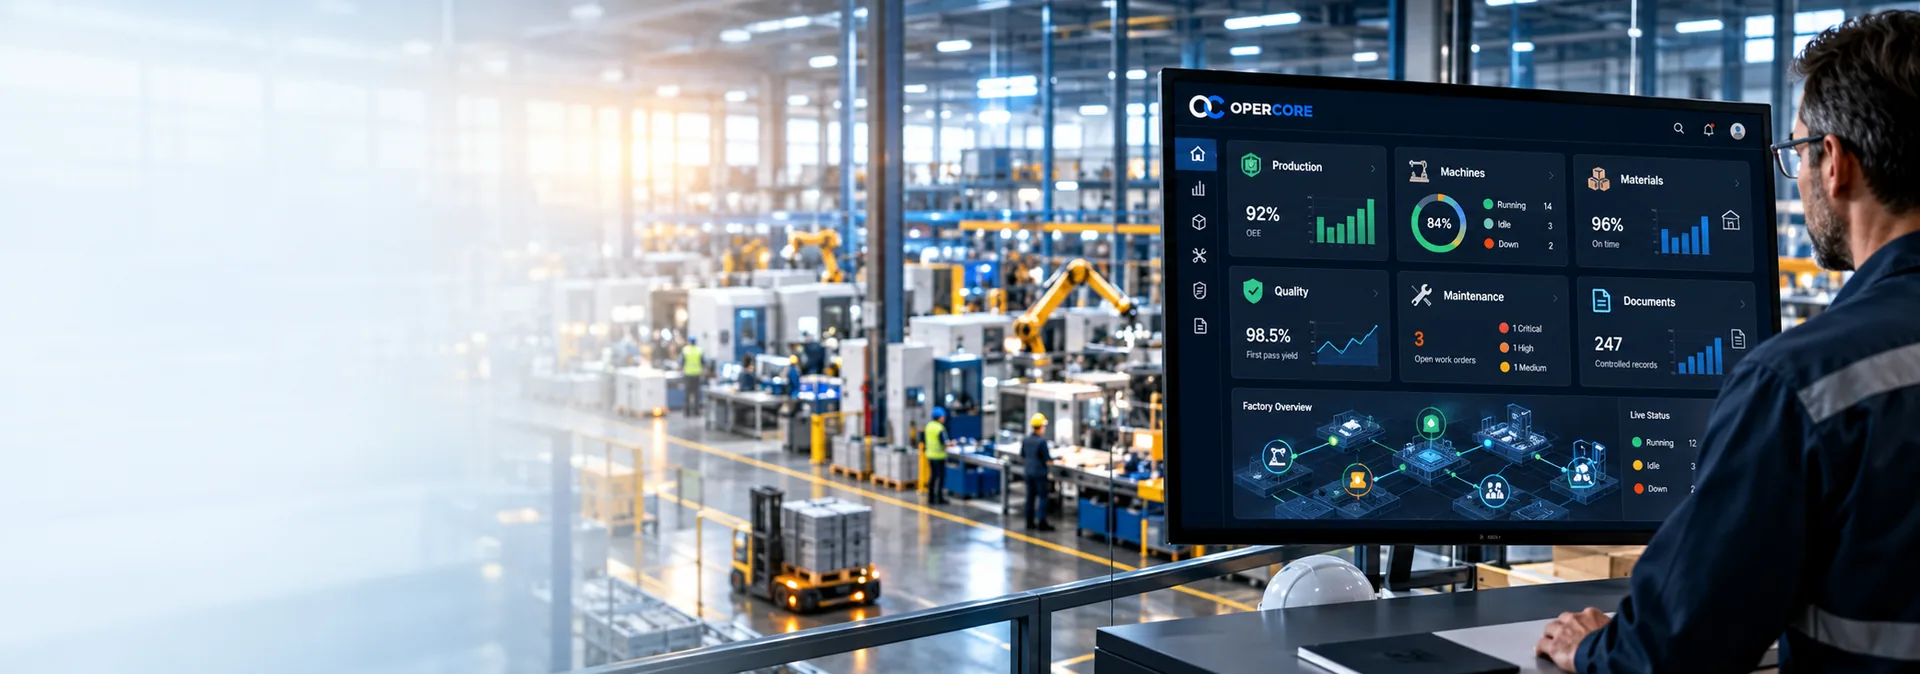
OPERCORE — Connects Operations is our flagship manufacturing operations platform. Its planning direction is human-first: helping planners understand workloads and relevant operational conditions, evaluate possibilities and remain responsible for the applied schedule.
OPERCORE proposes. The planner decides.
The intended result is better connected operational decisions—not an autonomous scheduling system that runs a factory on its own. Any detailed product capabilities and integration claims should be verified against the implementation before publication.
Frequently asked questions
What are the main constraints in production planning?
Typical constraints include equipment availability, bottleneck capacity, qualified staffing, tooling, material readiness, setup and changeover requirements, maintenance, inspection capacity, approved documentation and operation dependencies.
What is finite-capacity scheduling?
Finite-capacity scheduling attempts to place work within the available capacity of relevant resources while considering existing commitments. It can produce a more realistic sequence than loading work without capacity limits, but it still depends on correct resource, time and readiness data.
How can manufacturers improve the accuracy of production planning times?
Compare engineering standards with historical production orders and physical observations. Investigate setup, cleaning, cycle-time, downtime and reporting differences before updating planning data through the appropriate process.
Does a late production order always require replanning?
No. A planner should assess effects on downstream operations, critical resources and delivery commitments. Small deviations can sometimes be absorbed without changing the schedule, while a short delay at a constraint may require immediate action.
Is overtime a reliable way to recover lost production capacity?
Sometimes, but it is not unlimited capacity. Overtime depends on the necessary staffing and support resources, fatigue considerations, quality requirements and applicable working-time laws or agreements.
Can one operator supervise several machines?
In certain approved processes, yes. The decision depends on cycle characteristics, supervision requirements, skills, safety, process controls and company procedures. It should not be assumed as a universal staffing rule.
Does production scheduling software replace the planner?
No. Software can support visibility, capacity calculations, scenario evaluation and communication. The planner and responsible operational teams must still evaluate trade-offs, authorizations and actual factory conditions.
Conclusion: Build schedules that the factory can actually execute
The problem with many manufacturing schedules is not that they lack detail. It is that they are detailed representations of incomplete assumptions.
Realistic planning starts with the factory's limiting resources, verified process times, qualified staffing, material and engineering readiness, and the true dependencies between operations.
It accounts for setup and changeover work, makes appropriate room for normal variation, and uses reliable shop-floor reporting to show when execution is diverging from the plan.
It also requires judgment. Not every delay demands replanning, and not every recovery option is acceptable simply because it fits on a planning board.
The best production schedule is not the one that looks perfect on a screen. It is the one the factory can realistically execute—and the team can manage responsibly when reality changes.
Capar Labs helps manufacturers strengthen production planning, operational processes and connected information through practical consulting and digital technology.
Editorial note: Examples and calculations are fictional. Legal requirements vary by jurisdiction and employment arrangements. Standards and technical references provide context, not evidence of Capar Labs or OPERCORE certification or product conformity.
About Capar Labs
Capar Labs is a manufacturing technology company and end-to-end digital transformation partner. Our Manufacturing Insights combine practical manufacturing and process expertise with independent industry research to help manufacturers make better operational decisions.
OPERCORE
Connect planning, production and quality with OPERCORE
OPERCORE brings together production planning, shop-floor execution, material management, quality and operational workflows in a connected environment.
 Capar Labs