Manufacturing Data Silos: How to Connect Planning, Production and Quality
Why production, planning and quality see different operational facts—and how manufacturers can connect reliable information across their workflows.
Capar Labs18 min readManufacturing operationsDataQuality
A production planner checks the schedule and sees an order for 1,000 components due to ship on Friday. Production reports that all 1,000 pieces have been manufactured. But when the warehouse prepares the delivery, only 930 are available for release.
Where are the other 70?
Quality has placed them on hold pending inspection. The information exists, but it has not reached everyone who needs it. Sales may have confirmed a delivery date based on the planned quantity. Planning may have already reserved capacity for the next order. Production may believe the job is finished, while Quality and the warehouse are working from a different definition of finished.
Nobody necessarily entered a false number. The departments are looking at different parts of the same manufacturing reality.
This is what manufacturing data silos look like in daily operations. They create uncertainty between what was planned, what actually happened, what passed inspection and what can genuinely be delivered.
Connecting manufacturing information is not simply about joining software systems. It is about making sure the right people can see, trust and act on the same operational facts.
1What is a manufacturing data silo?
A manufacturing data silo exists when important information is isolated, inconsistent or difficult to use across the people and processes that depend on it.
The information may sit in different applications: enterprise resource planning (ERP), manufacturing execution (MES), quality management (QMS), warehouse systems, maintenance applications, engineering tools or machine-control systems.
But silos also exist inside a single application. Two departments may use different status definitions, maintain separate spreadsheets, or update an order at different times. An ERP and an MES might both have correct records within their own responsibilities, yet still leave employees uncertain about the current state of an order.
Consider a few common manufacturing questions:
Is the material physically in stock, reserved for another order, awaiting inspection or approved for use?
Is a production order finished because the machine stopped, because the operator reported completion, or because all required quality checks passed?
Does the latest drawing revision apply to the order already running, or only to orders released after an engineering change?
Is a machine available according to the schedule but unavailable because Maintenance has taken it out of service?
If the answers require multiple phone calls and spreadsheet checks, the problem is not merely missing information. It is missing operational context and connection.
The US National Institute of Standards and Technology (NIST) has studied the challenge of connecting design, manufacturing and inspection information through a digital thread. Its research makes an important distinction: information can exist across lifecycle stages without being completely linked or readily usable together. See NIST's digital-thread research and its study of design-to-inspection information integration.
Planning
Quantity and timing scheduled for production.
Production
Actual pieces and shop-floor progress.
Quality
Inspection, holds and accepted output.
Inventory
Finished goods genuinely available for delivery.
2Why manufacturing information becomes disconnected
Most factories do not deliberately design disconnected processes. Silos grow gradually as the business changes.
A warehouse adopts a system suited to stock management. Planning maintains a spreadsheet because the available software does not reflect real shop-floor constraints. Quality adds inspection records. Engineering controls drawings in another application. Maintenance uses its own work-order process. Each decision can make sense locally.
The difficulty appears when one activity depends on another.
For example, a planner may see enough material in inventory while the warehouse knows the material is not yet released. A production supervisor may receive an updated drawing by email while the original version remains linked to the active order. Quality may record a hold that is visible to its team but not to the people preparing shipment.
Three underlying causes appear repeatedly:
Different definitions
Departments disagree about what available, completed or released actually means.
Different timing
Information moves by shift reports or manual exports, so decisions use data that is already old.
Unclear ownership
No one is explicitly responsible for which system maintains a status, revision or result.
Different definitions. Departments disagree about what a status such as available, completed or released actually means.
Different timing. Information is transferred by shift reports, manual exports or end-of-day updates, so decisions are made using information that is already old.
Unclear ownership. No one is explicitly responsible for which system maintains a material status, drawing revision, production result or quality disposition.
These issues are organizational as much as technical. NIST's work on information governance for smart manufacturing emphasizes consistent, repeatable and trustworthy handling of industrial data. Connecting applications without resolving conflicting definitions can simply spread the confusion faster.
3One production order, three different answers
ILLUSTRATIVE PRODUCTION ORDER
Three different answers. One manufacturing reality.
Planned1,000Scheduled output
Manufactured1,000Produced quantity
Released930Accepted for next step
70 pieces on quality hold. A hold is not automatically scrap; disposition is still pending.
Take an illustrative order for 1,000 components.
Perspective
Recorded quantity
What it means
Planning
1,000 scheduled
The intended production output
Production
1,000 manufactured
The quantity physically reported as produced
Quality / release
930 accepted
The quantity currently approved for the next step or shipment
The remaining 70 pieces are on quality hold. They are not automatically scrap: they may still require inspection, investigation, rework or a formal disposition.
All three numbers can be correct. The failure happens when someone presents one of them as the answer to a different question.
Sales needs to know the quantity that can genuinely be promised or delivered. Planning needs to know whether the order is still consuming capacity or requires additional work. Production needs to understand the outstanding activity. Quality needs to preserve the distinction between a finished operation and an accepted product.
A connected workflow should make these distinctions visible without forcing employees to guess which department's number is the latest.
This is a stronger goal than putting 1,000, 1,000 and 930 on the same dashboard. The information must include its meaning, status, timing and relationship to the order.
4The real cost of disconnected manufacturing data
The most visible consequence of a silo is often wasted administrative effort. Employees spend time checking records, making calls, exporting reports and reconciling numbers.
The deeper cost is uncertainty in operational decisions.
Planning becomes less dependable
Schedules look achievable until a missing constraint appears.
Quality arrives too late
A hold that does not reach production or shipping can let work continue.
Employee trust declines
Teams build their own spreadsheets when the system disagrees with the factory.
Improvement is harder to measure
Yield, downtime and lead time cannot be compared if definitions differ.
Planning decisions become less dependable
A schedule based on incomplete material, machine or quality information may look achievable even when an important constraint is missing. Planners then have to rebuild the plan after the problem becomes visible.
Quality decisions arrive too late
If a nonconformance or hold does not reach the relevant production, planning and inventory workflows, another operation may begin or a shipment may be prepared before the restriction is understood.
Employee trust declines
When operators and supervisors repeatedly discover that the system disagrees with the factory, they build their own records to compensate. These spreadsheets or informal notes may solve an immediate problem, but they create yet another version of the information.
Improvement becomes harder to measure
A factory cannot evaluate schedule adherence, yield, downtime or lead time consistently if departments use different event times, quantities or definitions.
The cost does not have to appear as a dramatic system failure. It can accumulate through small delays, repeated checks, avoidable waiting and decisions made with incomplete context.
5Connect the complete manufacturing chain—not only planning and production
01Customer demand
02Engineering readiness
03Material availability
04Production planning
05Shop-floor execution
06Quality disposition
07Finished inventory
08Delivery
Manufacturing is a sequence of dependent decisions and activities. A connected information flow should reflect that sequence.
Several supporting controls interact with this chain, including equipment maintenance, staffing and competence, tooling, and controlled documentation.
Consider what the relevant teams need to know:
Activity
Essential information that must remain connected
Sales and order management
Customer demand, order changes, required quantities and delivery commitments
Engineering
Approved product definition, drawings, revisions, routings and manufacturing instructions
Purchasing and inventory
Material identity, available quantity, allocation and quality-release status
Production planning
Realistic capacity, sequence, constraints and intended order dates
Shop-floor execution
Actual progress, material consumption, produced quantities, interruptions and deviations
Quality
Required inspections, results, holds, rework and release decisions
Maintenance and equipment
Relevant availability restrictions, condition and service status
Finished goods and shipping
Accepted stock, traceable inventory and actual shipment status
This does not mean every company must put every function into one application. It means the relationships and decisions across functions must be coherent.
An established reference for thinking about business-to-factory information exchange is the ISA-95 / IEC 62264 family. Its relevance is not that a factory needs a particular software vendor, but that manufacturing operations and business systems have distinct responsibilities that must communicate clearly.
6Connect planned, actual and approved information
01 / PLANNED
What we intend to do
Schedules, routings, quantities
02 / ACTUAL
What actually happened
Execution events, material use
03 / APPROVED
What can proceed
Quality release, material readiness
These records are related, but they are not interchangeable.
One of the most useful ways to design connected manufacturing data is to distinguish three views of an order.
Planned: What the organization intends to do. This includes demand, materials, production routing, scheduled operations, expected quantities and timing.
Actual: What happened during execution. This includes start and finish events, material use, output, downtime, deviations and recorded results.
Approved or released: What the responsible people or functions have accepted for the next action. This may include engineering release, material release, quality disposition and authorization to ship.
These are related but not interchangeable.
A machine producing 1,000 pieces does not automatically mean 1,000 acceptable pieces are ready for delivery. Material being in a warehouse does not mean it has passed required controls. A document being available does not prove it is the approved revision for a particular production order.
NIST describes the broader challenge of linking as-designed, as-planned, as-executed and as-inspected information. That research perspective is useful because manufacturing decisions depend on relationships between these views, not on any one record in isolation.
A good connected workflow also preserves history. If an order is rescheduled or a drawing is revised, users may need to know both the current state and what was applicable at the time work was performed.
7Make operational restrictions visible before they become problems
Information integration is not only about reporting results after something happens. It should also help employees recognize when work cannot proceed as expected.
Take four common restrictions:
Materials
Arrival does not guarantee inspection, release and physical availability.
Engineering
A revised drawing or instruction may still be awaiting approval.
Machines & tooling
A machine can look free in a calendar and still be unavailable.
Quality
A hold must influence production, inventory and shipping decisions.
Materials. Raw material is expected tomorrow, but arrival does not guarantee it will be inspected, released and physically available when production needs it.
Engineering. A revised drawing or manufacturing instruction is still awaiting approval. The relevant order may not be ready to start, depending on the company's procedures.
Machines and tooling. A machine appears free in a planning calendar but is unavailable because of maintenance, qualification, servicing or another restriction.
Quality. A batch or component is placed on hold. Its status must influence subsequent production, inventory and shipping decisions according to the approved process.
Connecting these signals does not mean software should independently decide how to reorganize an entire factory.
For example, a system can show that a scheduled operation is at risk, identify the related orders and make possible alternatives easier to evaluate. The planner can then consider customer commitments, downstream work, available resources and applicable restrictions before deciding what to change.
The purpose of connected information is to support accountable human decisions, not to hide operational consequences behind automation.
8Give every important record a clear owner
Manufacturers sometimes respond to fragmentation by trying to establish one giant database as the master record for everything.
That is not always necessary or desirable.
A more practical question is: Which system or responsible function owns each type of information, and how is that information made available to others?
For example, a company might retain customer orders and purchasing information in ERP, engineering definitions in a document or product-lifecycle system, actual execution records in a manufacturing operations system, and formal quality decisions in an established quality workflow.
In another company, some of those functions may already live together.
What matters is that the arrangement is understood. A production order should not acquire two competing completion statuses without an agreed explanation. A shop-floor interface should not silently maintain a separate material availability figure that can drift away from authoritative inventory records.
Tulip's published guidance for ERP/MES integration makes a related point: existing external systems and operational applications can each be authoritative for different information, provided their responsibilities are explicit and the information is connected for the relevant workflow.
Useful questions for each shared record include:
Who is authorized to create or change it?
What does each status mean to the next department?
When is an update needed: immediately, at a defined event, or through a controlled periodic transfer?
How are errors, failed transfers and corrections detected and handled?
Can the user tell when the information was last updated and which order, item or batch it refers to?
This is how organizations move from disconnected numbers toward dependable operational information.
9Shop-floor reporting must fit the way people actually work
Technology adoption often succeeds or fails at the point where an employee is expected to capture information.
Production operators are responsible for manufacturing products safely and correctly. Reporting is essential, but it should not require navigating several unrelated screens or repeating information that already exists in an approved order.
Where appropriate, the work interface should already know the production order, relevant operation, applicable instructions and expected material. The employee should be able to confirm or record the actual event: starting an operation, consuming a material batch, completing a quantity, reporting a deviation or recording a required quality check.
The reporting method might be a fixed workstation, shop-floor terminal, tablet or suitable mobile device, depending on the environment and applicable requirements.
Some events can be captured from equipment or scanners. Others require a person's observation or confirmation. Automation can reduce repetitive work, but it cannot automatically establish the truth of every physical action.
Make correct reporting the easiest reasonable way to do the job.
This requires training, clear responsibility, practical interface design and feedback from the employees who will use the workflow every day.
10Turn connected records into useful operational intelligence
Once manufacturing data is connected and credible, managers can ask better questions.
Instead of simply viewing a schedule, they can compare what was planned with what has actually happened. Instead of treating production output as finished-goods availability, they can understand how much is accepted, awaiting checks or restricted. Instead of reviewing downtime without context, they can assess its effect on active operations and future commitments.
Examples of useful operational measures include:
Question
Relevant evidence
Are production orders progressing as planned?
Scheduled operations versus actual starts, completions and outstanding work
How much manufactured output is usable?
Produced, accepted, rejected and held quantities with clear definitions
Why did an order miss its target?
Material constraints, maintenance restrictions, production events and quality outcomes
Are material delays affecting future work?
Required dates, supplier status, inventory availability and release status
Can we trust our delivery commitment?
Accepted available quantities, remaining operations and realistic capacity
Manufacturing KPI frameworks such as ISO 22400 reinforce the importance of consistent definitions when measuring manufacturing operations. The exact KPI set should be selected to support the factory's decisions, not because every available number needs a dashboard.
Connected data is also a foundation for more advanced analysis and AI. But sophisticated analytics cannot compensate for unreliable event records or contradictory material and quality statuses. The first priority is credible operational evidence.
11How to start connecting manufacturing data without disrupting the factory
Improvement is more manageable when it begins with a real operational decision rather than an ambition to integrate every system at once.
Step 1 — Select one high-value problem
Choose a recurring situation that matters to the business: delivery promises based on incomplete order status, quality holds not visible to planning, or material availability that requires manual verification.
Define what a successful decision should look like. For example: Before confirming a shipment, can Sales and the warehouse reliably see the quantity that is actually released?
Step 2 — Follow the complete workflow on the shop floor
Walk through how the information is created and used. Observe an order from planning through execution, inspection and inventory. Record the places where employees must phone someone, re-enter data or consult separate spreadsheets.
Do not start by assuming that the problem is always a missing API. Sometimes the real cause is a poorly defined process or an unclear status.
Step 3 — Agree on meanings and ownership
Define the identifiers, states and responsible functions needed for the selected workflow.
For example, distinguish manufactured, inspection pending, on hold, accepted and available to ship if those are meaningful stages in the company's process.
Step 4 — Connect the necessary information and actions
Make the relevant order, material, production and quality information available to the people who use it. Keep the existing system owners where appropriate, and ensure the transfer or shared view preserves identity, timing and status.
Build the workflow around what employees need to accomplish, not around the technical connections themselves.
Step 5 — Test with real operating situations
Run representative cases: a material hold, a quality rejection, a late operation, a machine becoming unavailable and an approved document revision change.
Verify that the affected teams understand the same situation and that no one can mistake a planned quantity for released finished goods.
Step 6 — Measure and improve
Look at whether the change reduced manual reconciliation, improved information timeliness, prevented inconsistent statuses or made decisions easier to explain. Expand into other workflows only after the first one proves useful.
This approach reflects a broader lesson from manufacturing integration practice: the purpose of integration is to make a specific business process work better, not to collect as many system connections as possible.
12Common mistakes when trying to eliminate data silos
Replacing systems before understanding the process. A new platform cannot correct a confused definition of order completion or material release by itself.
Building dashboards before establishing trustworthy records. A visually attractive dashboard can reproduce incomplete or contradictory information at greater speed.
Duplicating records without defining authority. Copying the same material, order or status into several places creates new opportunities for disagreement unless updates and ownership are controlled.
Connecting everything in one large project. Integration scope grows quickly when every department and historical exception is included at once. Prioritize workflows that remove concrete operational friction.
Ignoring operators and supervisors. A solution that looks excellent in a conference-room demonstration may fail when employees are under production pressure.
Assuming automation should make every decision. Information can support constraint checks and recommendations, but operational responsibility and required approvals still matter.
13Where Capar Labs and OPERCORE fit
At Capar Labs, we approach connected manufacturing as both an operational and a technology challenge.
That can involve assessing the way departments exchange information, improving the underlying workflows, defining data ownership and integrating existing systems. The right solution is not always to replace the software a manufacturer already uses.
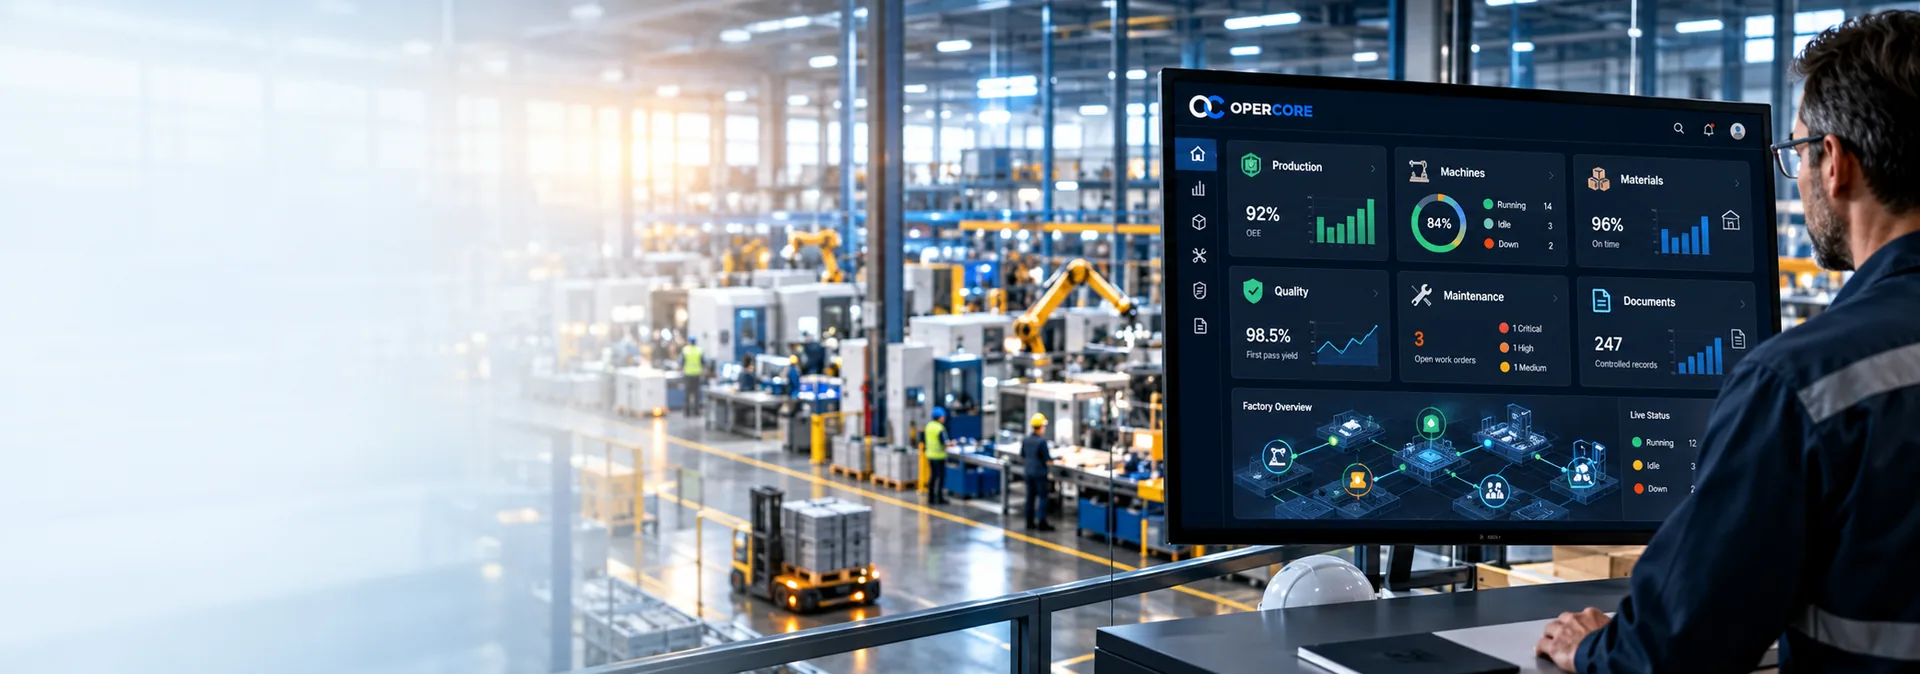
OPERCORE — Connects Operations is Capar Labs' manufacturing operations platform, designed around connected operational workflows and reliable manufacturing information. Its direction reflects the same principle discussed throughout this article: production, planning, materials, quality and relevant supporting activities should not be treated as unrelated islands.
Capar Labs' consulting services are broader than OPERCORE. Manufacturers can work with Capar Labs on manufacturing and process improvement, digital transformation strategy, industrial data and systems integration independently of adopting the platform.
Software capabilities, integration scope and any regulated-environment requirements should always be assessed against the actual implementation and intended use; a connected application alone is not proof of operational accuracy or compliance.
Frequently asked questions
What causes data silos in manufacturing?
Common causes include separate systems, conflicting status definitions, manual transfers, delayed updates, inconsistent identifiers and unclear ownership of information. Silos can also exist within a single software system when departments maintain different interpretations of the same process.
What is the difference between ERP and MES in manufacturing?
ERP commonly supports business planning, purchasing, inventory and order-management activities, while MES or manufacturing operations systems focus more closely on execution and operational records. The exact boundary depends on the software and how the company has implemented it. The important issue is whether necessary information moves reliably between business planning and factory execution.
Does every manufacturing system need to be replaced with one platform?
No. Separate systems can remain appropriate when they have clear responsibilities and exchange the information required by employees and business processes. A connected operational experience matters more than forcing every function into a single database.
Is real-time data always necessary?
Not for every record. A machine restriction or quality hold affecting immediate decisions may need rapid visibility, while other information can be exchanged at defined points in the workflow. The required speed depends on the decision, risk and operational process.
Can small and mid-sized manufacturers benefit from connected data?
Yes. Even a small factory can experience delays when planning, material availability, production reporting and quality releases rely on disconnected spreadsheets or verbal updates. A focused improvement to one important workflow can be more valuable than a large software replacement.
Does connected manufacturing data mean AI will run production planning?
No. Better information can support analysis, identify constraints and help evaluate possible changes, but planning decisions still need human ownership and appropriate controls. Connected data supports judgment; it does not remove accountability.
Conclusion: Connect decisions, not just databases
Manufacturers rarely lack information. More often, the information exists in different places, means different things to different departments, or reaches people too late to support the decision in front of them.
Connecting planning, production and quality begins by clarifying what each team needs to know and which records can be trusted. It continues by connecting customer demand, engineering readiness, material status, operational execution, quality decisions and finished-goods availability.
The goal is not to collect every possible data point or force an entire factory into one application. It is to create a dependable view of what is planned, what actually happened, what is approved and what needs attention next.
When manufacturing information reflects the reality of the factory, employees spend less time reconciling numbers and more time making informed operational decisions.
Explore Capar Labs' Manufacturing & Operational Excellence and Systems, Integration & Implementation services, or learn about OPERCORE — Connects Operations.
Capar Labs is a manufacturing technology company and end-to-end digital transformation partner. Our Manufacturing Insights combine practical manufacturing and process expertise with independent industry research to help manufacturers make better operational decisions.
OPERCORE
Connect planning, production and quality with OPERCORE
OPERCORE brings together production planning, shop-floor execution, material management, quality and operational workflows in a connected environment.
 Capar Labs